Products · Fixed
Infra-View® infrared boiler / furnace thermometer
A permanently mounted infrared sensor that reads the temperature of the combustion gas through any boiler or furnace penetration and delivers it to the control room as a 4–20 mA signal. Continuous, non-contact, and with nothing in the gas stream to erode or burn out.
Documents
- Infra-View® literature sheetPDF · 130 KBThe two-page overview: how the sensor reads hot CO₂, the 250°F to 3,000°F range, the cooled and purged jacket, and suggested installation locations on a boiler.
- Measuring FEGT in industrial furnaces (application note)PDF · 6.2 MBWhy furnace exit gas temperature matters, contact versus non-contact methods, the factors that skew a reading, and how Infra-View® is applied.
- Installation, operation and maintenance manualOn requestIssued with each unit and on request for existing installations, so the current revision always goes out.
- Calibration and maintenance guide / NIST certificateOn requestSensor calibrations and rebuilds are a service we provide; the guide and a NIST-traceable certificate are issued on request.
Principles of operation
Burning coal, gas, oil, lignite, biomass or waste produces hot carbon dioxide. The Infra-View® detector is a thin-film thermopile behind a spectral filter that passes only the infrared band emitted by hot CO2 and blocks every other wavelength. Because it responds to the gas and not to the flame, the tube walls or the slag, the reading is the gas temperature across its field of view — average, high or low, as you configure it.
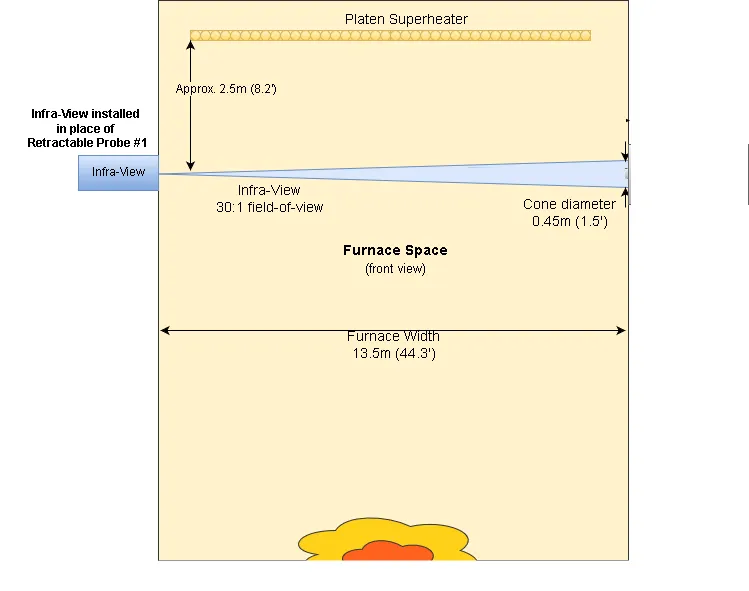
The optics look into the furnace through a 30:1 field of view (a 3 ft spot at 90 ft). The signal is a linear 4–20 mA loop, fully sub-scalable, so the DCS sees temperature directly.
Specifications
- Temperature range
- 250°F to 3,000°F; higher end temperatures available.
- Detector
- Thin-film thermopile with a CO₂-band spectral filter; responds to the hot gas, not to surfaces or flame.
- Field of view
- 30:1 field of view (a 3 ft spot at 90 ft).
- Output
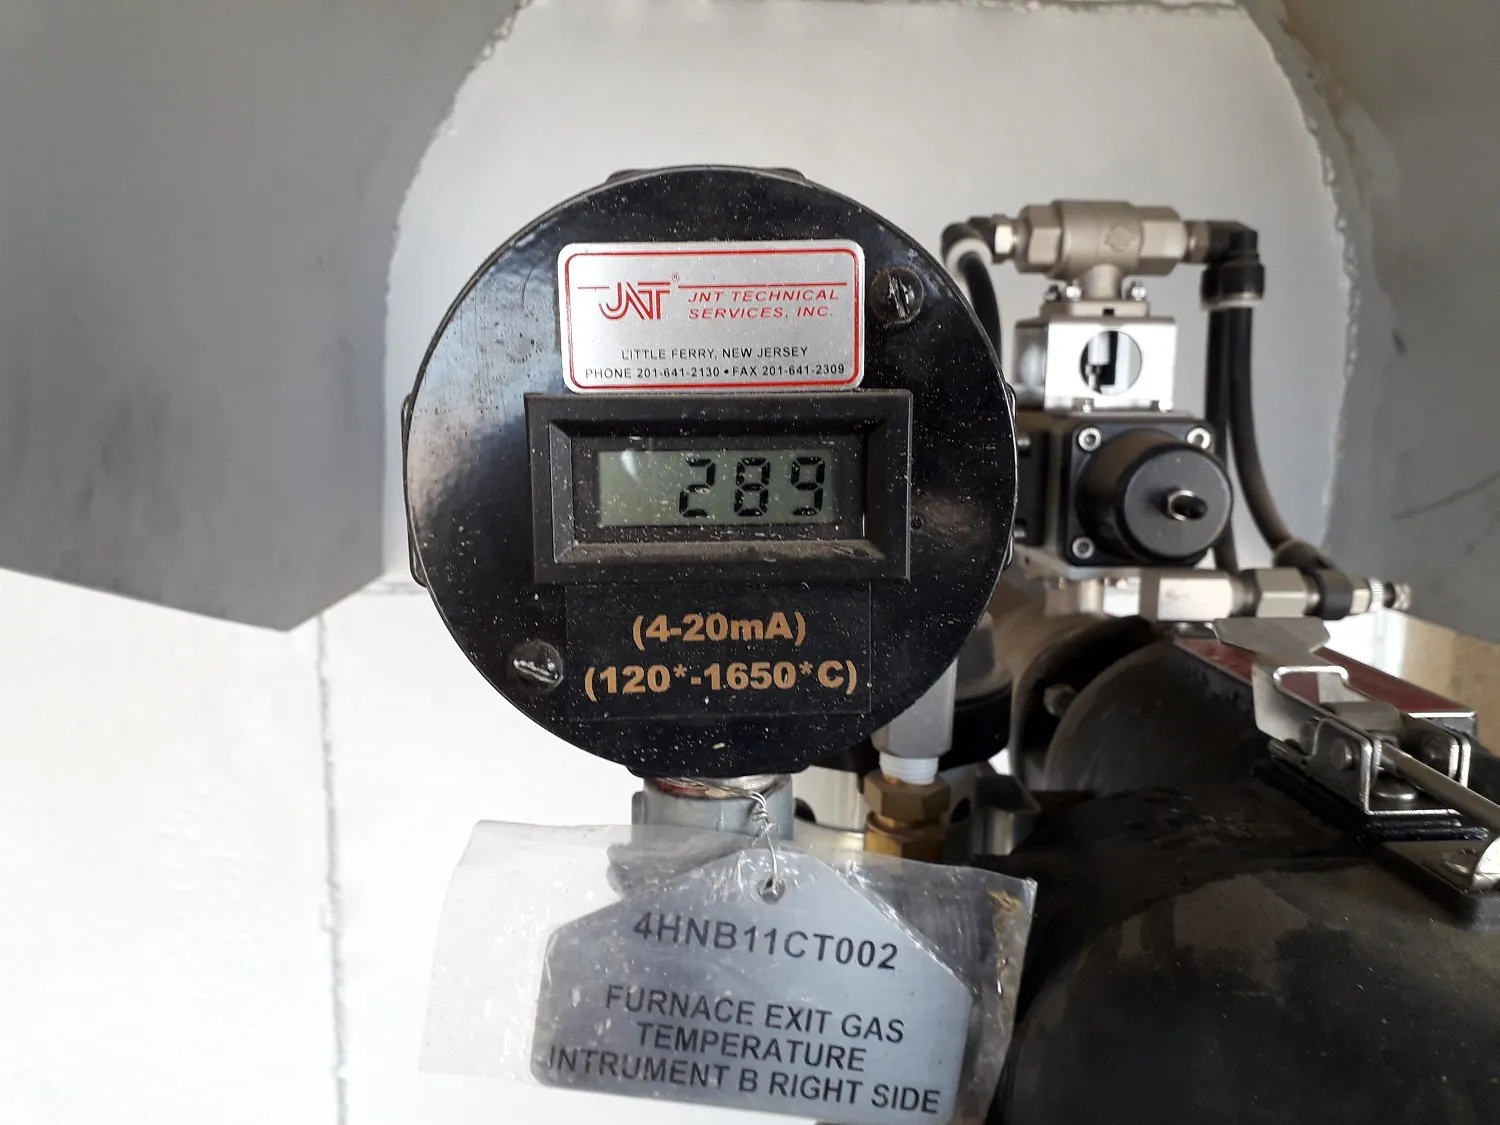
- 4–20 mA, loop powered (0–20 mA available), fully sub-scalable.
- Response time
- 100 ms response (600 readings per minute).
- Mounting
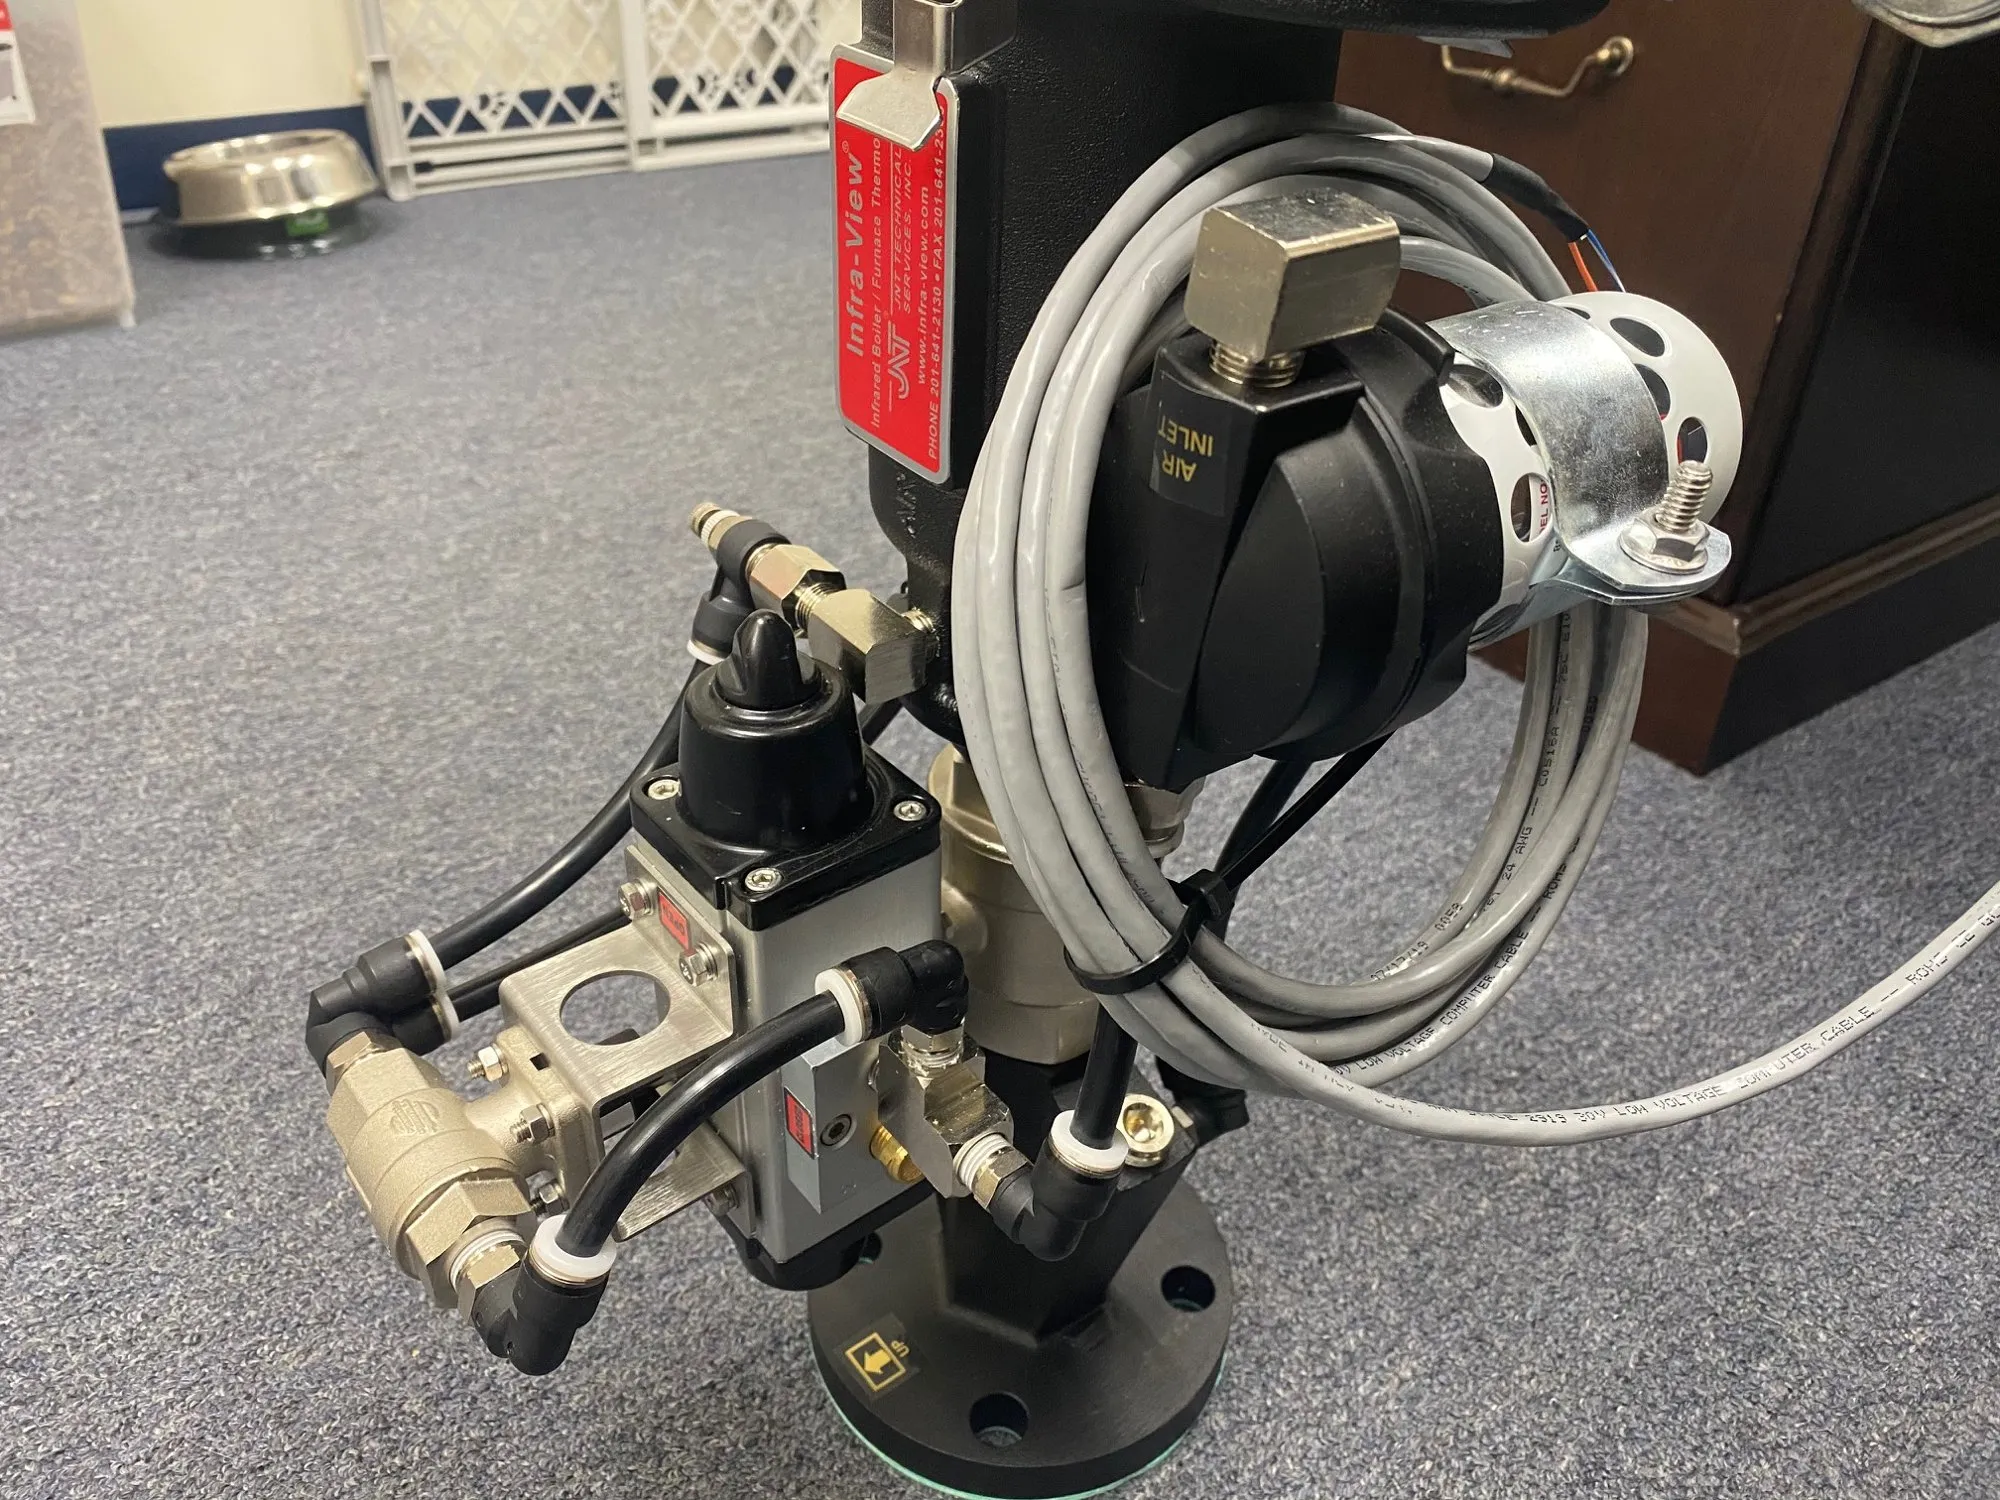
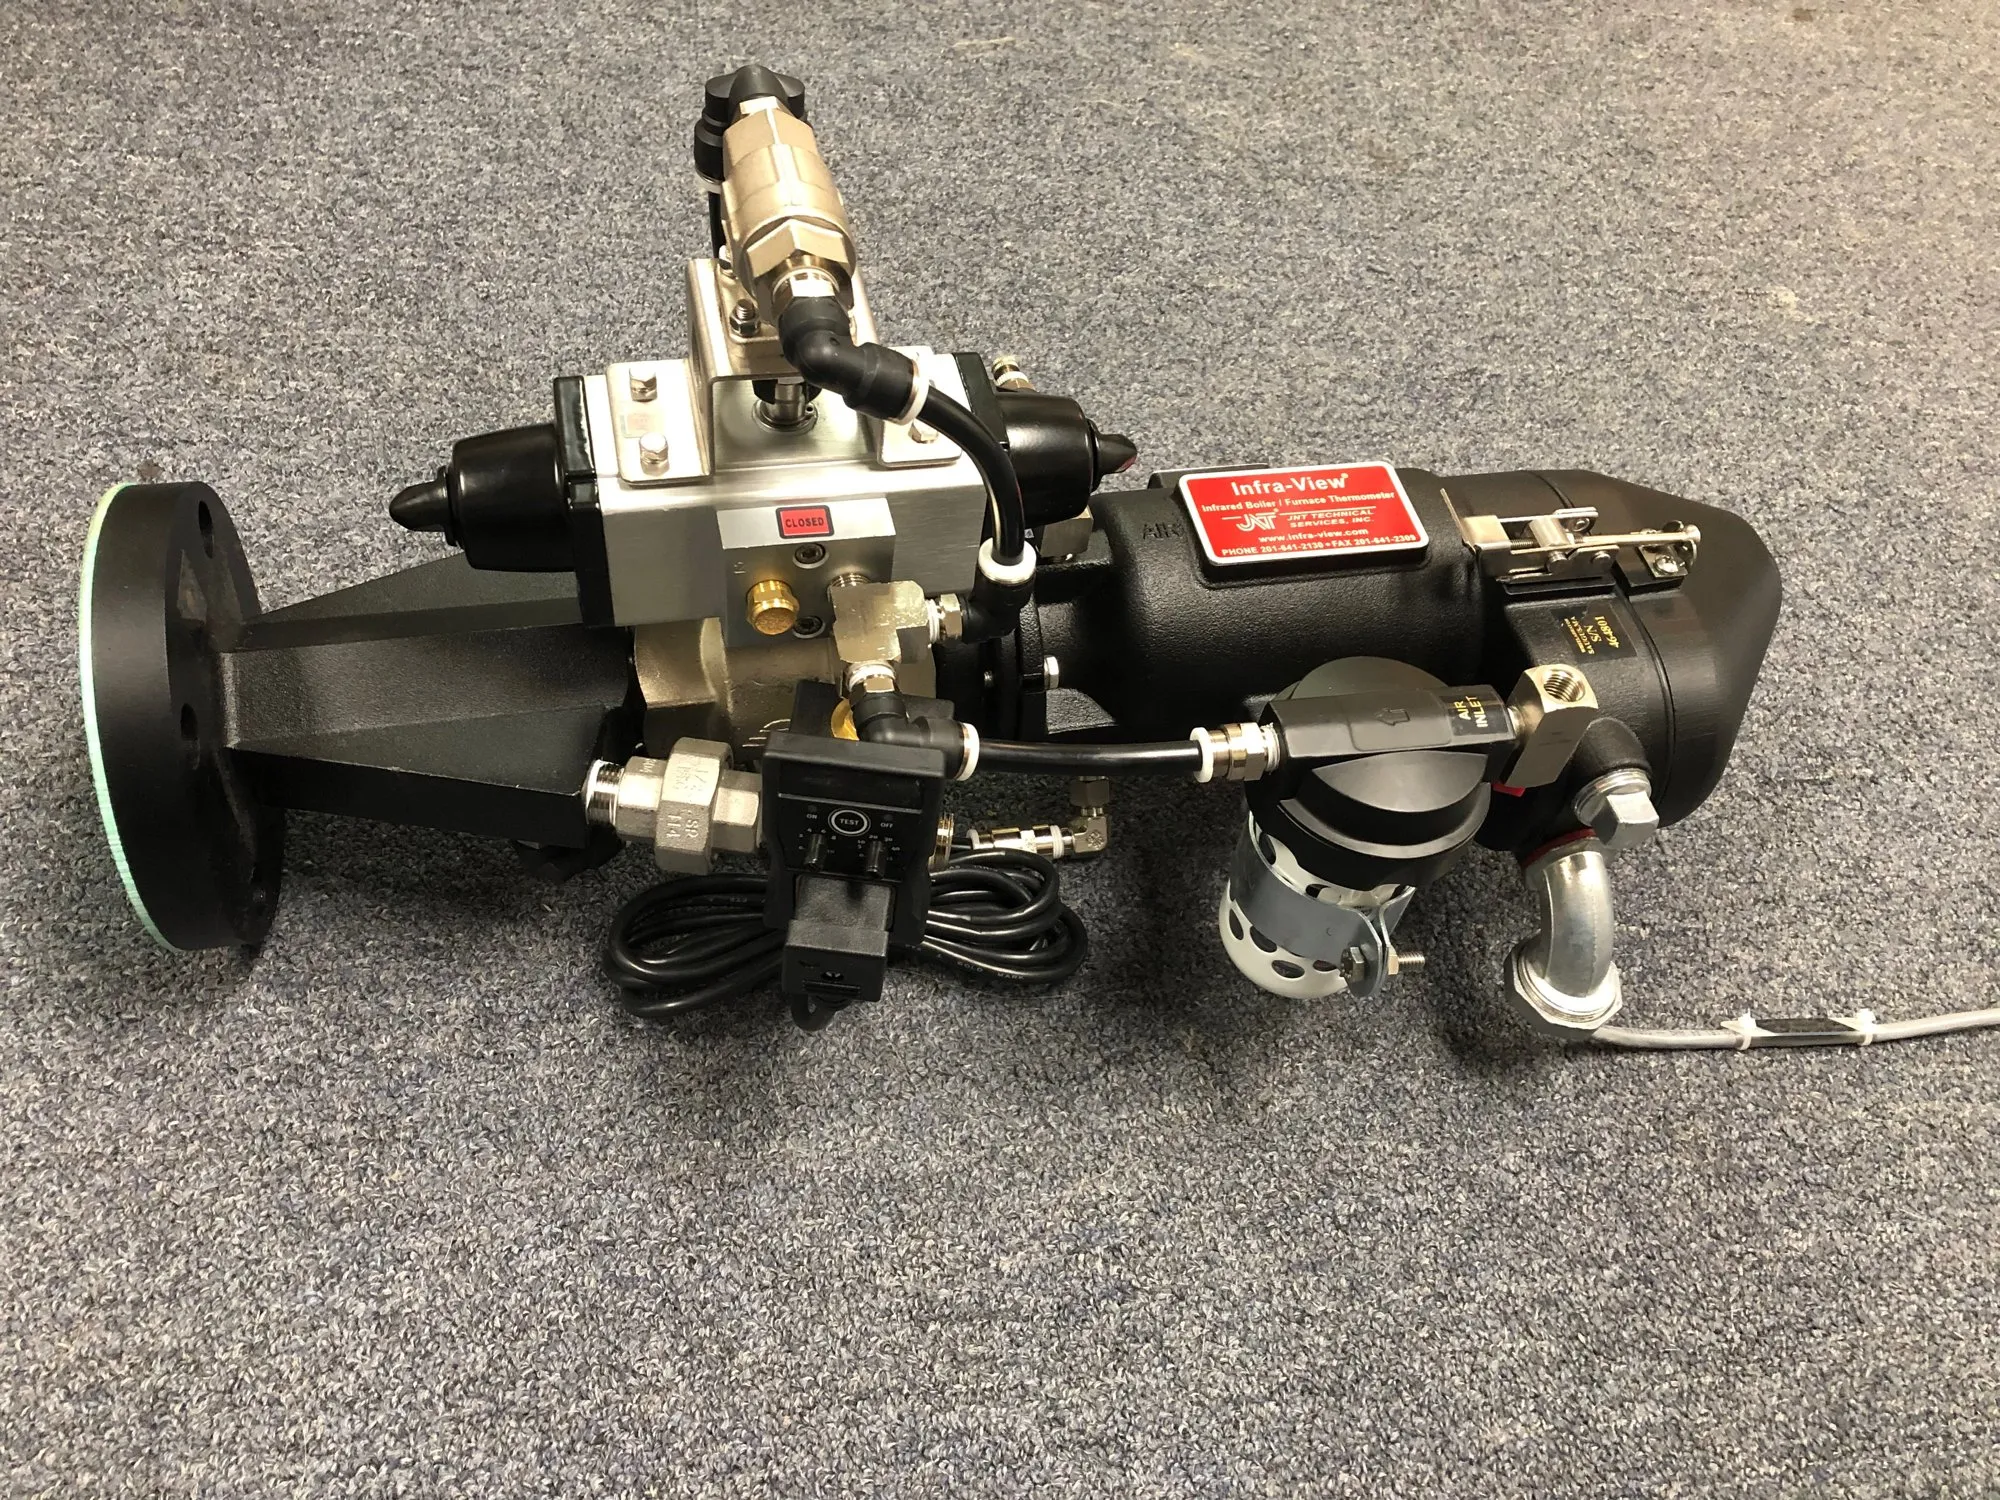
- Flange-mounted on any port, door or penetration — factory-assembled with the protective jacket.
- Cooling and purge
- Air-cooled, purged and filtered protective jacket, factory assembled — customer-supplied compressed air.
- Wiring
- Two-wire shielded signal cable into a 4–20 mA loop from the DCS, a digital or an analog recorder.
- Certification
- CE certified; nist-traceable calibration certificate on request.
Each unit is calibrated for the fuel and the boiler it is going into before it ships. The installation, operation and maintenance manual is issued with the unit and on request.
Applications and installations
What plants use the reading for
- Startup and shutdown — watch the furnace come up to temperature and hold within limits.
- Slagging and fouling — a rising exit gas temperature at constant load is heat that is not reaching the water walls; see it before the sootblowers do.
- Heat transfer — confirm the effect of a burner change, a tilt setting or a cleaning cycle.
- Emissions-control protection — hold the FGD or SNCR inlet below the temperature the equipment is rated for.
- Combustion optimization — a continuous FEGT signal is the feedback a tuning project needs.
Where it is installed
Fossil, biomass and waste-to-energy boilers, industrial furnaces and process heaters, in the United States and abroad. Typical positions are the furnace exit, the nose arch, ahead of the superheater and at the economizer outlet; the literature sheet shows suggested locations, and we recommend positions for your unit from your boiler drawings.
A retractable thermocouple or an HVT probe gives a point reading that erodes in the gas stream. Infra-View® reads from outside the wall, continuously, and stays in service through the run.
Technical background
The application note covers why furnace exit gas temperature matters, contact and non-contact ways of measuring it, the factors that skew a reading (emissivity, soot and ash, sensor position) and how Infra-View® is applied. It is on this site as a page and as a PDF.